


Why Aluminum Is Hard to Weld: How a Modern Spot Welder for Aluminum Solves It
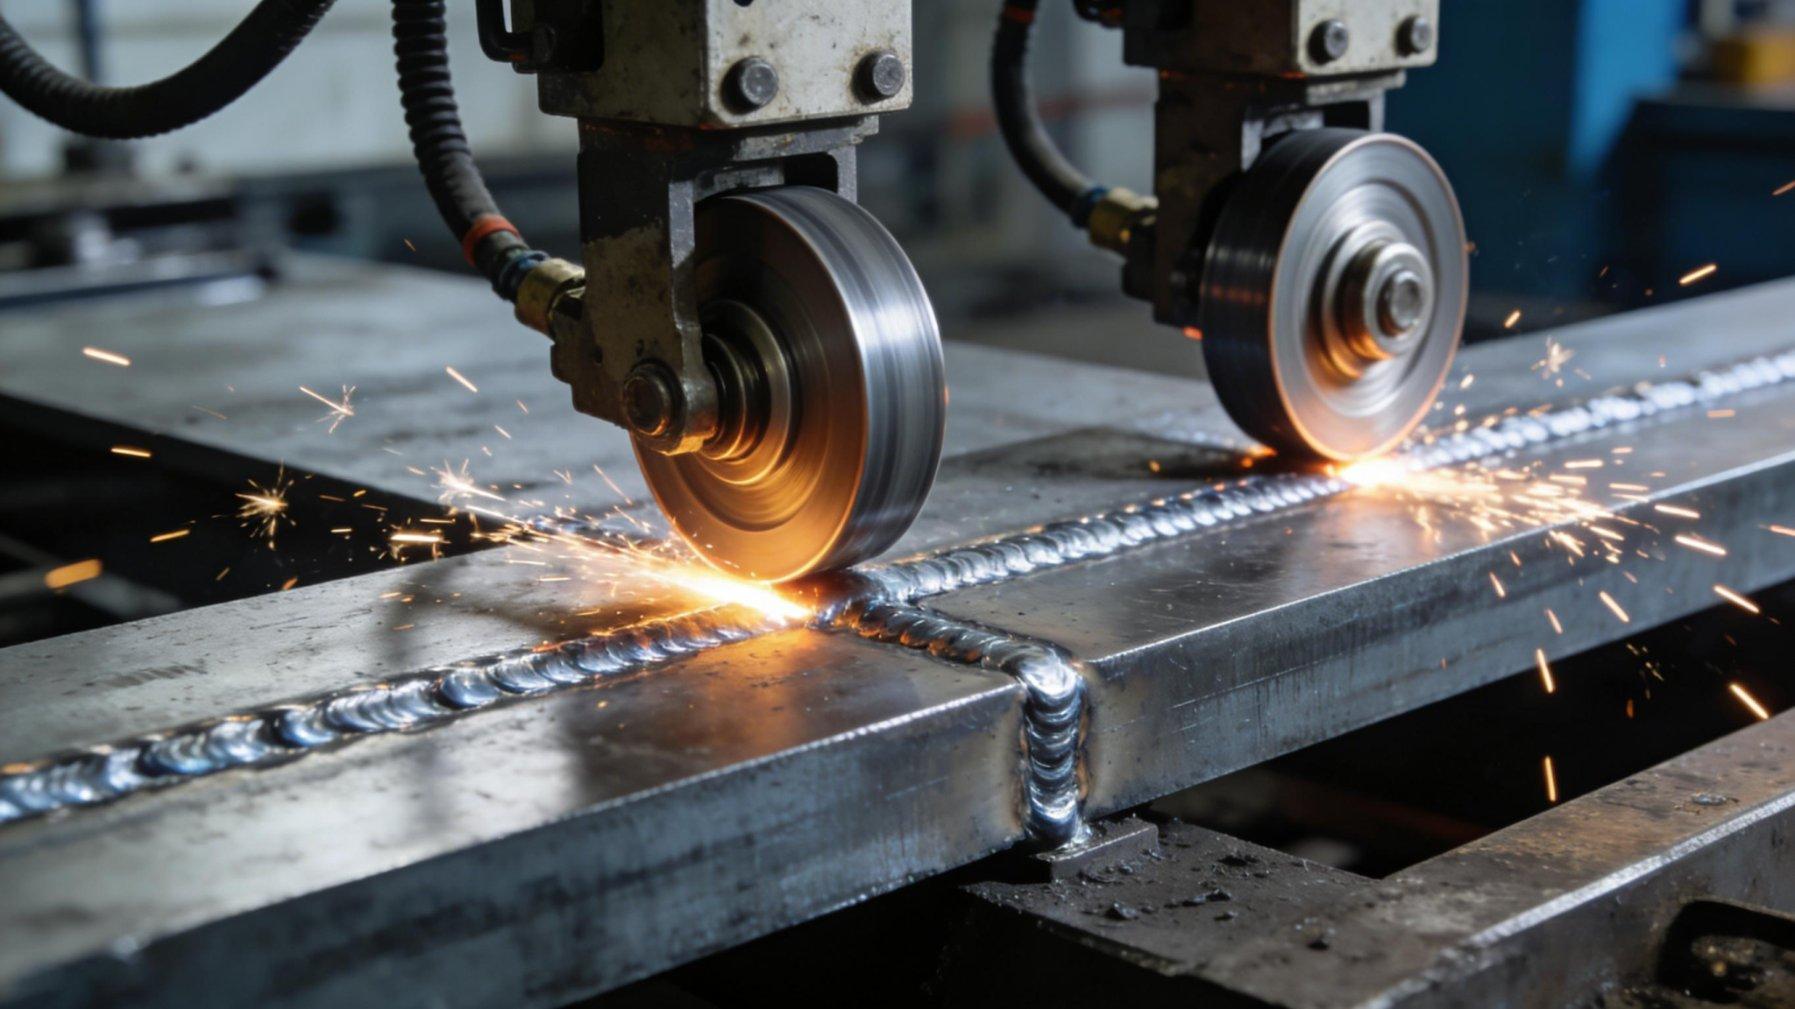
Automakers keep adding aluminum to every new platform, chasing lighter bodies and longer electric range, and every one of those aluminum panels has to be joined somehow. Engineers who try the process quickly discover that a spot welder for aluminum faces physics that mild steel never presented: a stubborn oxide skin, extreme thermal conductivity, and a narrow window between a cold joint and a burned-through panel. Yet aluminum spot welding is now a mature, reliable production process used on high-volume body lines. This article explains the metallurgical challenges and the machine features that overcome them.
The Oxide Layer: A Ceramic Skin on Every Sheet
Aluminum exposed to air instantly grows a film of aluminum oxide, a ceramic that melts near 2000 degrees Celsius while the metal beneath melts at only 660. Electrically, the oxide is a high-resistance insulator, and its thickness varies with storage time, humidity, and surface treatment, which makes contact resistance unpredictable from one panel to the next. If the welding current cannot break through that film uniformly, the heat concentrates in patches and the nugget forms off-center or not at all. Successful aluminum welding therefore starts before the current flows: consistent surface preparation, controlled storage, and electrode force high enough to fracture the oxide mechanically at the contact point. Modern weld schedules often open with a short conditioning pulse designed specifically to disrupt the film and establish stable metal-to-metal contact.
Conductivity That Steals Your Heat
Aluminum conducts both heat and electricity far better than steel, roughly four times the thermal conductivity, and that generosity works against the welder. Heat races away from the joint into the surrounding sheet and into the water-cooled electrodes almost as fast as the current generates it. To outrun those losses, aluminum schedules use very high current delivered in very short times, often just a few cycles of the mains frequency. The margin for error shrinks accordingly: extend the time slightly and the heat spreads, producing a wide but shallow nugget with poor strength. This is why aluminum welding demands power supplies with fast current rise and precise timing, since a sluggish transformer simply cannot put enough energy into the joint before it escapes.
The Narrow Welding Window
Every material has a range of current and time settings that produce acceptable welds, and for aluminum that range is famously tight. Too little energy yields a small, weak nugget that fails peel testing; too much causes expulsion, where molten metal erupts from the joint and leaves voids behind. A further complication is electrode sticking: aluminum alloys with copper at welding temperatures, and the electrode can bond to the sheet surface, tearing the panel on opening or leaving copper contamination in the joint. Operators learn to recognize the warning signs, including spatter at the sheet surface and a harsh, crackling weld sound, but in production the real answer is equipment that holds parameters inside the window automatically rather than relying on human vigilance.
Machine Features That Tame Aluminum
Purpose-built aluminum welders combine several technologies to widen that narrow window. Medium-frequency direct current power supplies deliver the rapid current rise and exact pulse shaping that aluminum needs, with none of the waveform distortion of older AC machines. Servo-driven electrode force systems apply high, programmable pressure profiles that fracture the oxide and forge the nugget, adjusting within milliseconds as the weld progresses. Multi-pulse schedules let engineers program preheat, weld, and forge phases independently, tailoring the thermal cycle to each alloy and thickness. Closed-loop feedback monitors current and voltage every millisecond and trims the output in real time, compensating for the natural variation in oxide thickness between panels. Together, these features turn a temperamental process into a controlled one.
Electrode and Process Practices That Matter
Hardware choices reinforce what the machine provides. Copper-chromium-zirconium electrode alloys resist the alloying and softening that aluminum inflicts, lasting far longer than pure copper in this service. Larger tip faces than steel practice dictates help distribute the high current and reduce sticking, while frequent tip dressing keeps the face geometry consistent. Many shops standardize on a fixed weld count between dressings and track it with the controller's built-in counter. Surface cleanliness deserves equal attention: oils, drawing lubricants, and heavy oxidation all widen process variation, so panels should move from cleaning to welding on a defined schedule. With the right alloy, disciplined dressing, and clean stock, aluminum spot welding achieves the same process capability that steel shops take for granted.
Conclusion
spot welder for aluminum technology has turned one of manufacturing's trickiest joining tasks into a dependable production process. Fast MFDC power, servo force control, multi-pulse schedules, and real-time feedback conquer the oxide layer and the conductivity challenge together. For engineers moving into aluminum-intensive designs, the lesson is encouraging: respect the metallurgy, specify the right machine features, and aluminum spot welds will hold their own against any joint on the vehicle.
#AluminumWelding #SpotWelding #AutomotiveManufacturing #HeronWelder

 English
 Arabic
 French
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek
 Bengali