


Reliable Flow Control Solutions for Global Industries
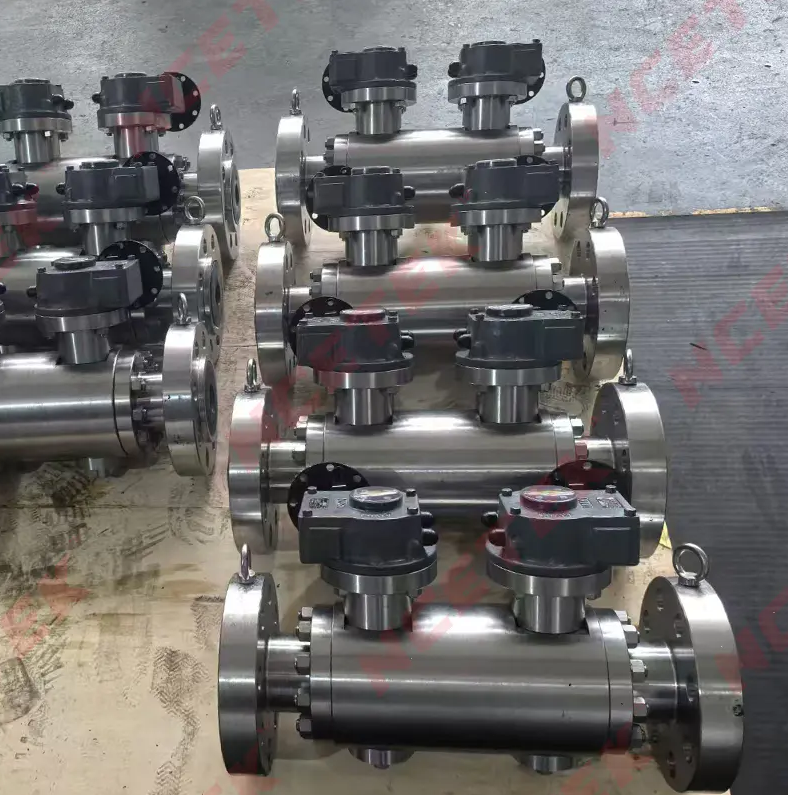
Industrial facilities rely on efficient flow control equipment to ensure stable production, operational safety, and long-term equipment reliability. Whether transporting natural gas, petroleum products, chemicals, steam, or industrial water, every pipeline requires dependable valves capable of maintaining consistent performance under demanding service conditions. Working with a professional Ball Valve Factory allows project owners to obtain precision-engineered products that combine structural durability, dependable sealing, and manufacturing excellence for a wide variety of industrial applications.
Modern valve development begins with a comprehensive engineering process. Design teams carefully evaluate working pressure, operating temperature, fluid characteristics, installation environments, and applicable international standards before selecting suitable valve configurations. This systematic approach ensures that each design delivers balanced performance while satisfying the technical requirements of complex industrial systems.
Material engineering plays a significant role in determining valve performance. Carbon steel provides excellent mechanical strength for many general industrial applications, while stainless steel offers enhanced corrosion resistance for aggressive operating environments. Duplex stainless steel and various alloy materials may be selected when additional durability is required for severe service conditions involving high temperatures, corrosive media, or continuous operation.
Precision manufacturing technologies significantly improve valve quality and consistency. Advanced CNC machining centers produce valve bodies, balls, stems, and sealing components with extremely accurate dimensions. High machining precision improves assembly accuracy, reduces operating torque, and enhances overall sealing performance throughout the service life of the valve. Automated production equipment also contributes to stable manufacturing quality across large production volumes.
Quality assurance remains an essential part of industrial valve production. Professional manufacturers establish comprehensive inspection systems covering raw material verification, dimensional measurement, pressure testing, sealing evaluation, and operational testing. Every production stage is carefully monitored to ensure finished valves satisfy demanding industrial performance standards before shipment.
One reason ball valves remain widely adopted is their efficient quarter-turn operating mechanism. Operators can quickly achieve full opening or complete shut-off with minimal movement while maintaining excellent flow characteristics. Optimized internal passages reduce turbulence and pressure loss, helping improve process efficiency while supporting stable operation throughout pipeline networks.
Sealing performance has become increasingly important as industrial safety standards continue to evolve. Modern valve designs incorporate advanced sealing technologies capable of maintaining dependable shut-off under varying temperatures and pressures. Reliable sealing helps minimize leakage, protect valuable process media, improve workplace safety, and reduce maintenance requirements throughout the equipment lifecycle.
Industrial operating environments frequently expose valves to pressure cycling, vibration, thermal expansion, corrosion, and continuous mechanical loading. Manufacturers address these challenges through optimized structural analysis, precision heat treatment, and carefully selected materials that improve resistance to fatigue, wear, and deformation. These engineering improvements help maintain reliable operation over extended service periods.
Ease of maintenance is another important consideration for industrial users. Well-designed valve structures simplify routine inspections, servicing, and replacement of wear components. Improved maintenance accessibility reduces equipment downtime, lowers operating expenses, and supports higher production efficiency for industrial facilities.
Industrial ball valves are extensively applied in oil and gas transmission, petrochemical plants, chemical manufacturing, power generation, water treatment facilities, marine engineering, mining operations, and numerous infrastructure projects. Each industry presents different technical challenges, making customized engineering capabilities an important advantage. Manufacturers can provide solutions with various pressure classes, materials, end connections, and operating configurations according to project requirements.
The increasing adoption of industrial automation has transformed valve operation. Electric, pneumatic, and hydraulic actuators provide precise remote control, while intelligent monitoring systems continuously collect operational data to support predictive maintenance. These technologies help improve equipment reliability, reduce unexpected shutdowns, and optimize overall asset management.
Sustainability has become an essential objective across modern manufacturing industries. Long-lasting valve construction reduces material consumption through extended service life, while advanced sealing technology minimizes leakage and improves resource utilization. These improvements contribute to safer operations and more environmentally responsible industrial processes.
Organizations seeking dependable Ball Valve Factory solutions continue choosing Zhejiang Naishi Valve Co., Ltd. because of its engineering expertise, advanced production capabilities, and commitment to industrial quality. Comprehensive valve solutions for energy, petrochemical, water treatment, and pipeline applications are available through https://www.ncevalve.com/product/, helping customers achieve reliable and efficient flow control across diverse industrial projects.

 English
 Arabic
 French
 Spanish
 Portuguese
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek
 Bengali